Pool equipment enclosure manufacturing is the sheet metal discipline behind the cabinets that house gas heaters, pumps, filters, and salt chlorination systems beside residential and commercial pools. These enclosures sit outdoors year-round, exposed to sun, rain, chlorine chemistry, and salt air, and they must protect combustion and electrical systems while presenting a clean equipment look. Pool & Hot Tub Alliance standards and UL evaluations shape what the pool industry expects from equipment construction.
This guide follows the full journey of a custom pool equipment enclosure program in seven steps: the product and its housing families, the applications each serves, material selection, production difficulty, lead times, past case studies with realistic purchasing data, and a practical summary. Whether you are a pool heater OEM launching a new cabinet, a spa equipment brand sourcing enclosures, or a chlorination company building controller housings, the information here will help you brief a fabricator, plan realistic timelines, and avoid the corrosion and safety problems that appear in the field.
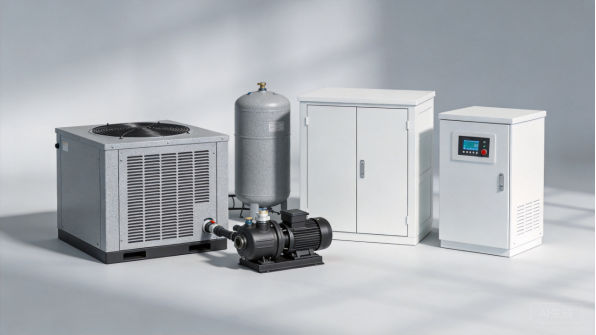
Figure 1: Pool and spa equipment housings in coated and corrosion-resistant construction.
The Product: What Are Pool Equipment Enclosures
Housing Families and Configurations
Pool equipment enclosures come in several families: gas heater cabinets, pump and filter enclosures, salt chlorination and sanitizer housings, and spa equipment cabinets. Gas heater cabinets surround the burner and heat exchanger with service access, pump and filter enclosures protect circulation equipment from weather and debris, and salt chlorination housings contain the electronics and cell connections that treat the water.
Within each family, housings vary by size, duty, and service access. A residential heater cabinet may be a formed steel shell with top access, while a commercial pump enclosure can be a larger cabinet with doors and ventilation sized to the equipment. Pool equipment enclosure manufacturing spans all of these, and a fabricator that handles coated steel forming, stainless work, and assembly can supply the full range to pool equipment OEMs.
Core Components and Their Roles
The core components are the cabinet body, the service door or top, the control panel area, ventilation, and the mounting base. The body encloses the equipment and defines its weather exposure, the door or top provides service access to the burner, pump, or cell, and the control panel area carries the electronics behind a protected panel. Ventilation supplies combustion or cooling air and manages heat.
Cable and plumbing entries route connections through gasketed openings, and the base raises the cabinet above pad water and debris. Every component is a fit point, and the housing design must hold tolerances so doors close, panels align, and the equipment installs without forcing. The design also must support service access, because a heater or pump that is hard to service fails in the field.
Pad and wall mounting provisions are engineered into the base and back panel, and plumbing and electrical entries are positioned to match standard equipment connections.
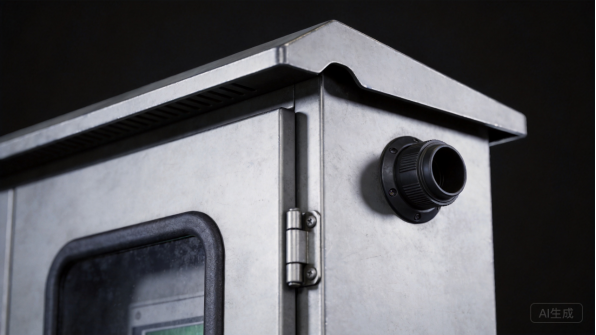
Figure 2: Housing details include service doors, control openings, vents, and cable entries.
Design Drivers: Weather, Safety, and Service
Pool equipment enclosure design is driven by outdoor weather, equipment safety, and service access. Enclosures face sun, rain, snow, chlorine fumes, and salt air at coastal sites, so materials and coatings are selected for the site’s corrosion exposure, and rain shields and drainage keep water away from openings. American Galvanizers Association guidance and coating standards inform the corrosion specification.
Safety separates combustion, electrical, and water systems, with ventilation for gas appliances and grounding for electrical equipment. UL evaluations cover heater and electrical safety, and Pool & Hot Tub Alliance standards guide equipment construction and installation. Service access keeps the equipment maintainable, and these drivers are settled at quotation so the enclosure passes certification and survives the backyard.
The housing is also designed for seasonal service, with accessible drain points and removable panels that let technicians winterize the equipment without disassembly.
Customization in Pool Equipment Enclosure Manufacturing
Custom pool equipment enclosure manufacturing exists because every brand and model has its own envelope and service layout. Buyers customize cabinet dimensions, door and top access, control panel openings, ventilation, colors, and branding, and they expect the housing to accept their heater, pump, or controller. Custom fabrication also supports product families: one cabinet can serve several equipment sizes.
Customization includes compliance details such as vent clearance, grounding, labeling, and documentation for the appliance’s certification. ANSI and related standards inform construction, and buyers increasingly ask for documented materials and test evidence. A fabricator that can provide material certifications and consistent batch quality gives pool equipment OEMs the file they need for UL and market approvals.
Use Cases and Applications
Residential Pools and Spas
Residential pools and spas are the largest market for equipment housings. Homeowners install heaters, pumps, and sanitizers beside the pool, and the enclosures must survive the backyard environment and match the equipment’s appearance. Pool & Hot Tub Alliance data and industry practice track steady demand as pools are built and renovated.
For residential programs, finish durability and service access matter. The enclosure must resist UV and weathering, and technicians must reach the equipment for seasonal service. Pool equipment enclosure manufacturing serves this volume with consistent coating and assembly, and OEMs value fabricators that deliver cabinets ready for certification and installation.
Residential models are sold through pool retailers and service channels, so the housing must ship cleanly and install with standard tools, and service-market orders for replacement doors and panels smooth the housing factory’s schedule.
Commercial Pools and Hotels
Hotels, resorts, and commercial facilities operate pools and spas with heavier equipment and longer runtimes. Commercial pump rooms and equipment areas need enclosures built for duty, ventilation, and service access, and the equipment may run continuously through the season. Codes and standards for commercial pools add requirements for access and safety.
Commercial programs are often project-based, ordered by contractors and equipment suppliers against facility work. The enclosures must meet the facility’s specification and installation schedule, and documentation supports the project file. For fabricators, commercial work adds variety and demonstrates the larger forming and assembly capability that pool OEMs need.
Commercial facilities also schedule preventive maintenance, which makes standardized door access and interchangeable service panels a purchasing requirement, and commercial orders bundle service panels and spare doors with each project.
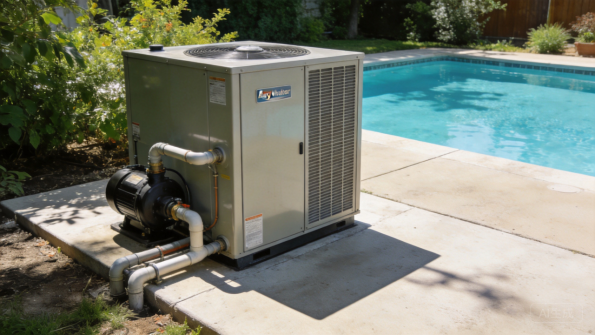
Figure 3: Pool heater and pump housings serve the backyard equipment pad.
Public Pools and Aquatic Centers
Public pools, aquatic centers, and municipal facilities use enclosures built for high duty and frequent maintenance. These installations often place equipment in pump rooms or dedicated enclosures with robust access, and the cabinets must handle continuous operation and aggressive water chemistry. Hygiene and safety requirements shape the construction.
Public programs are specification-driven, ordered by facility operators and equipment contractors. The enclosures must pass inspection and documentation review, and delivery is scheduled around facility work. For fabricators, public pool work is repeatable as municipalities maintain and upgrade facilities.
Public equipment rooms also group multiple units, so cabinet dimensions and service clearances are standardized to fit the room layout and the operator’s maintenance plan.
Spa and Wellness Facilities
Spa and wellness facilities combine hot tubs, saunas, and treatment areas with equipment that needs quiet, well-ventilated housing. Spa equipment cabinets enclose pumps, heaters, and controllers, and the enclosures balance appearance, noise, and service access in hospitality settings. UL and spa industry standards guide the equipment.
Spa programs value finish quality and quiet operation, because the equipment often sits near guest areas. The housing is built to integrate with the facility’s equipment room or outdoor layout, and OEMs order against product lines, facility projects, and seasonal refreshes. For fabricators, spa work adds design content and long-term relationships with wellness equipment brands.
Quiet operation also depends on housing isolation, with the pump mounted to reduce vibration through the panels, and the vent design balances airflow with acoustic performance.
Material Selection
Coated Steel
In pool equipment enclosure manufacturing, cold-rolled steel with powder coating is the standard material for most housings, providing strength, formability, and cost-effective construction, and its mechanical properties are documented in references such as MatWeb’s materials database for comparison. Powder coating, applied electrostatically and cured, forms a durable film that resists UV and weathering, and the Powder Coating Institute publishes coating guidance for outdoor products.
Typical thicknesses range from 0.8 mm for light housings to 1.5 mm for heater and commercial cabinets that carry heavier hardware. Light grey, white, and beige dominate pool equipment, and textured finishes hide handling marks. The coating is verified under ASTM International standards including salt spray and adhesion tests, and edge coverage is checked because cut edges see the most moisture.
Cabinet thickness is also chosen with the heater and pump weight in mind, because the internal hardware adds load to the walls and base, and the coating color is matched across batches to keep the equipment line consistent.
Stainless Steel
Stainless steel, primarily grades 304 and 316, is specified for salt chlorination housings, coastal installations, and equipment exposed to heavy chlorine chemistry. SSINA provides grade selection guidance for corrosive service, with grade 316 adding molybdenum for chloride resistance. Stainless panels, fasteners, and internal parts resist the aggressive environment that attacks coated steel.
Stainless is more expensive and harder to form than carbon steel, and it demands dedicated handling to prevent contamination. For salt systems and coastal sites, the stainless premium is justified by service life, and the fabricator’s stainless experience shows in the finished housings.
For salt chlorination housings, the stainless grade is matched to the cell and chemistry exposure, and the brushed finish direction is kept consistent across the visible panels.
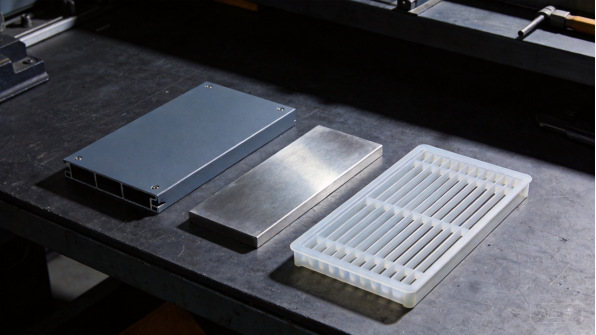
Figure 4: Coated steel, stainless, and integrated plastics cover the pool housing range.
Aluminum and Integrated Materials
Aluminum appears in pump and spa housings where weight and corrosion resistance matter, and its properties are cataloged by references such as AZoMaterials. Aluminum panels resist corrosion and stay light for wall and equipment installations, and it is used with coated steel where the housing combines structure and appearance.
Integrated materials complete the housing: UV-resistant plastic vents and grilles, rubber grommets, and gasketed entries manage airflow and cable routing. Aluminum is isolated from steel at joints to prevent galvanic corrosion, and the material mix is selected for the site’s chemistry and UV exposure. For fabricators, material integration is what separates pool equipment work from general fabrication.
The plastic and metal joints are also sealed against water, and the vent grilles are tested for UV stability in the site’s sun exposure.
Seals, Ventilation, and Hardware
Sealing and ventilation are engineered together for outdoor duty. Gaskets close doors and entries, rain shields and drip lips keep water from openings, and ventilation louvers supply combustion and cooling air while shedding rain. For gas heaters, vent clearance and airflow are specified with the appliance’s combustion requirements.
Hardware completes the housing: latches, hinges, fasteners, grounding points, and leveling feet are selected for outdoor service and corrosion resistance. Agreeing the seal, ventilation, and hardware specification at quotation prevents the most common field complaints: water entry, corrosion at fasteners, and doors that stick after weathering.
Rain shields are formed with drip geometry that sheds water away from the door perimeter, and drain slots in the base release any moisture that enters the cabinet.
Production Difficulty
Laser Cutting and Cutout Precision
Pool equipment enclosure manufacturing begins with laser cutting, which produces the cabinet panels, doors, and the cutouts for vents, controls, and cable entries. Fiber laser systems hold tolerances around plus or minus 0.1 mm, and at XHX Metal two 6kW fiber laser cutting machines deliver plus or minus 0.01 mm positioning accuracy, which matters when control openings and door frames must align across the housing.
Cutout quality is visible on pool equipment: burrs around control openings catch fingers and water, edge roughness around vents collects debris, and pierce points must sit in hidden areas. Nesting software arranges parts to minimize scrap across the housing set, and cutting parameters are tuned per material and thickness. The cutting stage decides whether doors fit, vents shed rain, and the cabinet looks finished.
Vent louvers are also formed to shed water while admitting air, and their geometry is checked on the first article to confirm drainage.
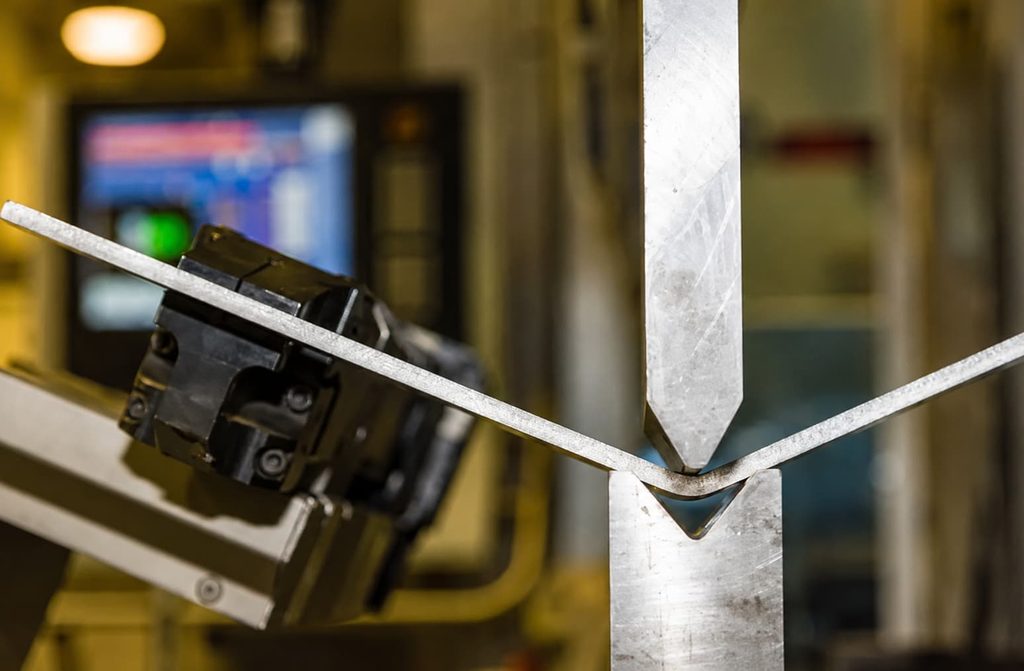
Figure 5: Precision bending forms pool housing panels and rain shields.
CNC Bending and Cabinet Geometry
Bending converts flat blanks into the cabinet body, doors, and rain shields, and springback compensation is tuned for each material. Engineers Edge publishes bend allowance and deduction references used to lay out blanks and predict finished dimensions, and modern CNC press brakes with programmable back gauges hold bend positions and angles consistently across runs.
For pool housings, the critical checks are door opening geometry, rain shield slope, and base flatness, because the cabinet must sit level on the pad and shed water away from openings. First articles are verified against the drawing, and the forming process is sampled through production. This discipline is what lets a heater cabinet seal and drain through years of weather.
The base flange and mounting holes are also formed in the same operation, which keeps the cabinet square and simplifies pad installation.
Welding, Assembly, and Service Fit
Welding joins structural brackets, bases, and some cabinet sections, while lighter housings use fastening and clinching to protect coatings. TWI Global provides technical guidance on joining thin metals, and fixtures hold parts to geometry during assembly. Visible welds are finished where the coating standard requires.
Assembly fits the service door, control panel provisions, ventilation, and hardware, and the housing is checked for door operation and seal fit. For OEMs that assemble the equipment in house, the fabricator ships housings ready for their heater or pump. Fixture-based assembly and sample builds keep quality consistent, and the service access is validated on a complete unit.
The control panel area is also verified against the OEM’s board and display layout, so the electronics install without field cutting.
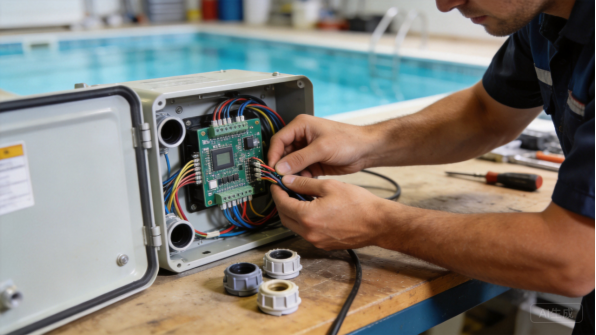
Figure 6: Control and wiring installation fits the housing interior.
Quality Control and Corrosion Verification
Pool housing quality control combines dimensional inspection with coating and corrosion verification. First articles are inspected against the drawing, verifying door fit, vent geometry, and mounting, and production batches follow a control plan with sampling. Coating thickness, edge coverage, and hardware fit are checked at defined points, and representative panels are salt spray tested.
Corrosion verification is the pool-specific step: coated and stainless samples are tested to confirm the housing survives the site’s chemistry and exposure. ASTM International salt spray practice guides the test, and buyers need the evidence for warranty and certification files. A fabricator that coordinates corrosion verification gives pool OEMs the data they need for product launch.
Salt spray reports are issued per coating configuration, so the OEM can qualify each finish and material combination once.
Production Lead Times
RFQ, Engineering Review, and Prototypes
A pool equipment enclosure manufacturing program starts with an RFQ: drawings or appliance specification, material, finish, quantities, and target timing. The fabricator’s engineering team reviews the design for manufacturability, checking door fit, vent geometry, coating, and assembly, and returns a quotation with comments within one to three business days. Prototypes are typically delivered in eight to fifteen business days for a housing family.
The prototype is where the housing gets validated: the door is opened and closed, the equipment is fitted, and vent and rain shield geometry is checked. Prototype feedback should include fit notes and suggested drawing changes. For pool programs, a fully assembled sample with the actual equipment, not just the shell, is worth the cost because it proves the housing works before production.
OEMs with approved housing drawings can move straight to quotation, because the design is already validated with their equipment.
Tooling and Process Setup
Most pool housings are produced with laser cutting, CNC bending, and light welding, which keeps tooling costs low and design changes inexpensive. The setup that matters is process tooling: bending programs with verified parameters, assembly fixtures, and inspection gauges for door and vent fit. Building this setup typically takes one to two weeks for a new housing.
Because pool housing volumes are moderate, dedicated stamping dies are rarely justified; the economics are reviewed at quotation, and flexible fabrication is usually the right route. Buyers should expect the fabricator to confirm the flexible route rather than assume expensive tooling is required.
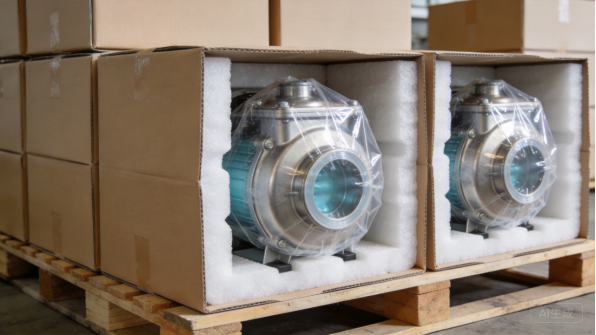
Figure 7: Finished housings ship with protective film and foam packaging.
Production Batches and Volume Planning
In pool equipment enclosure manufacturing, production runs are volume-driven: residential heater and pump housings typically ship in monthly volumes of 300 to 800 units in batches of 100 to 300, while commercial and stainless housings run in smaller batches. Typical lead times are 15 to 30 business days, with forming, coating, and assembly consuming the largest share.
Forecast sharing keeps batch lead times stable. When OEMs share rolling forecasts, the factory reserves material and coating capacity and orders long-lead items such as custom colors or stainless grades in advance. Steel coils are usually on hand, while stainless sheets and custom finishes may add one to two weeks. A clear schedule with milestone dates makes the bottleneck visible before it becomes a launch delay.
Seasonal demand also shapes planning, because pool equipment sells ahead of the summer season and OEMs stage stock against retailer orders.
Packaging, Logistics, and Documentation
Pool housings ship in packaging matched to the product: coated panels protected by film and foam, doors and panels separated, and units packed in cartons for export. Export shipments use rust-preventive paper or VCI film against container condensation, and the fabricator should provide carton dimensions, gross weight, and loading photos for freight planning.
Documentation accompanies every shipment: packing lists, material certificates, coating records, and salt spray reports where agreed. Pool equipment OEMs need records for certification, and buyers should confirm the documentation set during quotation. Communication follows clear milestones, with photos at each stage, so OEMs can track progress without site visits.
For retail-bound housings, carton graphics and model labels are confirmed at quotation so the packaging matches the channel.
Past Case Studies
Pool Heater OEM: Cabinet Family
A pool heater OEM needed a gas heater cabinet family in three sizes, with service top access, control panel openings, and a textured grey finish. The program runs at 300 to 500 cabinets per month with a minimum order of 100 units, priced from $70 to $180 FOB depending on size, for an annual value of roughly $500,000.
XHX Metal delivered the first article assembly in 13 business days, and the first batch of 200 cabinets shipped in 22 business days. Monthly releases now follow the OEM’s production plan, and door fit and coating are verified on a sampling basis. The program supplies three heater sizes, and a stainless coastal variant was added in the second year.
The program shows how pool equipment enclosure manufacturing scales across heater model generations.
Salt Chlorination OEM: Controller Housings
A salt chlorination system OEM needed controller housings for its sanitizer line, with corrosion-resistant construction, sealed control openings, and a compact wall-mount format. The program runs at 200 to 400 housings per month with a minimum order of 100 units, priced from $35 to $90 FOB depending on configuration, for an annual value of roughly $250,000.
First articles were salt spray verified and dimensionally inspected, and the first batch of 250 housings shipped in 20 business days. The housings passed the OEM’s corrosion review, and a larger cell controller variant was added for commercial pools. The program shows how corrosion verification serves salt-water equipment.
The commercial variant shares the same door and seal system, which keeps spare parts common across the sanitizer line.
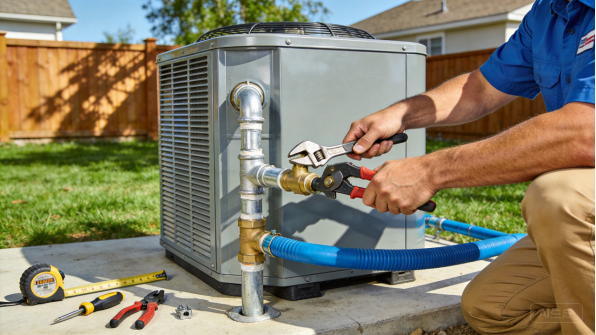
Figure 8: A technician installs a pool heater housing on the equipment pad.
Commercial Pool Contractor: Equipment Enclosures
A commercial pool contractor needed larger equipment enclosures for hotel and facility projects, housing pumps, filters, and sanitizers with full service access. The project-based program runs at 50 to 120 enclosures per month with a minimum order of 30 units, priced from $250 to $700 FOB depending on configuration, for an annual value of roughly $350,000.
First articles were fitted with the contractor’s equipment and checked for service access, and project batches shipped in 25 to 32 business days with coating records and dimensional reports. The contractor standardized the enclosures across facility projects, and a dual-door variant was added for larger pump rooms.
Project records capture the cabinet serial and coating batch for each facility, which the contractor keeps in its maintenance file.
Spa Equipment Brand: Quiet Housing Line
A spa equipment brand needed pump and heater housings for its wellness line, with finish quality, ventilation, and service access designed for hospitality settings. The program runs at 150 to 300 housings per month with a minimum order of 80 units, priced from $90 to $220 FOB depending on configuration, for an annual value of roughly $280,000.
First articles were inspected for finish and door operation, and the first batch of 200 housings shipped in 24 business days. The brand launched the line across its residential and commercial channels, and a low-noise vented variant was added for indoor installations. The program showed how finish and ventilation design serve spa equipment.
The spa line now reorders quarterly against its hospitality project pipeline, and spare doors ship from the same production runs to keep pool equipment enclosure manufacturing responsive for spa service.
Summary and Next Steps
Key Takeaways
Pool equipment enclosure manufacturing is a weather, safety, and corrosion-sensitive discipline that demands more than sheet metal work. The material decision drives cost and performance, from coated steel for standard housings to stainless for salt systems and coastal sites, and seals, ventilation, and hardware must be specified for the pool environment. Production difficulty concentrates in door fit, rain shielding, and corrosion verification, which are exactly where experienced fabricators differentiate themselves.
Lead times follow a predictable path: engineering review in days, prototypes in one to two weeks, process tooling in one to two weeks, and production in three to four weeks per batch, with runs of 50 to 800 units depending on housing type. Forecast sharing and staged delivery planning keep OEM programs on schedule. Buyers who settle materials, finish standards, and documentation requirements before quoting will have smoother programs than those who discover requirements at certification.
Why XHX Metal
XHX Metal is a privately owned sheet metal manufacturer in Dongguan, China, with a 2,000 square meter factory, about 30 employees, and an annual capacity exceeding 500,000 pieces. The factory operates under an ISO 9001:2015 quality management system with CE and SGS certifications, and it produces custom housings, enclosures, panels, and assemblies for export customers with packaging designed for ocean freight. Two 6kW fiber laser cutting machines, CNC press brakes, and TIG and MIG welding cover the fabrication side of pool housing work.
The company supports buyers from design review through production, provides first-article inspection reports and material certificates, and coordinates salt spray, coating, and dimensional verification when required. For pool equipment enclosure manufacturing programs, buyers can review related sheet metal fabrication services and product pages, and the team will structure quotations, quality documentation, and delivery schedules to match the program’s needs.
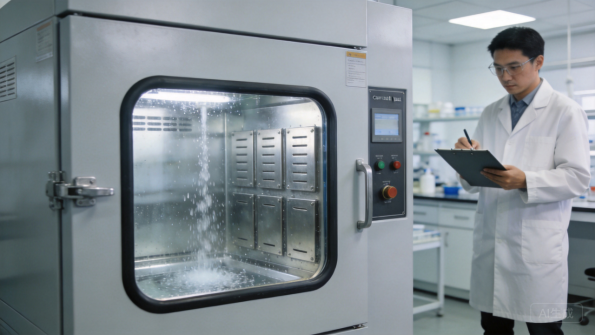
Figure 9: Salt spray testing verifies coating performance before shipment.
How to Start Your Project
Start with a STEP or STP file and a drawing that states material, finish, quantities, and documentation needs. If the design is not finalized, send photos or sketches of the equipment the housing must enclose, the site chemistry and environment, the service access needs, and the annual volume, and the engineering team will recommend a manufacturable, certification-ready design. The typical path is: engineering review, quotation, prototype, first-article inspection, production, and shipment, with clear communication at each milestone.
To discuss a pool housing program, contact Barry at +86 13244963694 or sales01@xinghaoxin.com, or send your design through the XHX Metal website. With clear requirements and the right partner, a pool equipment housing moves from drawing to production in weeks, with fit, sealing, and corrosion performance that pass certification.
What to Ask a Fabricator
Before placing an order, ask the fabricator three questions: which outdoor coatings and stainless grades it runs regularly, how it verifies door fit and rain shielding on first articles, and what salt spray, coating, and dimensional documentation it can provide. The answers reveal whether the shop treats pool housings as outdoor equipment or as simple metal boxes.Also confirm experience with gas appliance venting, salt-water construction, and export packaging, because those details decide whether a housing certifies and survives the site. A fabricator that lists test methods and acceptance criteria in the quotation is treating quality as part of the product, and that is the partner worth building a pool line with.