1. Product Overview: What a Server Rack Actually Is
1.1. What the 19-Inch Standard Means
A server rack is a standardized steel frame that holds servers, network switches, storage devices, power distribution units, and cable management equipment in one vertical structure. In the IT world the product is defined by the 19-inch standard: the mounting width is 482.6 mm, and the vertical mounting holes follow a grid called the rack unit or U, where one U equals 44.45 mm. Because most equipment is built to this grid, the frame must be square, rigid, and dimensionally consistent. If the rails are out of position, servers bind, switches hang out of place, and installation teams lose time on every rack. For a sheet metal manufacturer, this makes the server rack one of the most precision-sensitive products in the workshop.
1.2. Rack Types and Configurations
The product family is wider than most buyers expect. A two-post relay rack is an open frame with two vertical rails, used for network switches, patch panels, and lightweight telecom gear. A four-post open rack adds rear rails so long servers are supported at both ends. An enclosed server cabinet adds side panels, front and rear doors, a top, and a base, which controls airflow and keeps dust out. Wall-mount racks fit network closets, and compact cabinets serve edge computing sites. All of these share one manufacturing core: a precise steel frame with the correct mounting pattern.
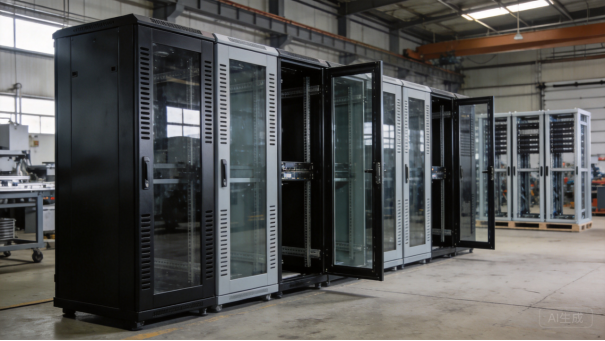
server racks and network cabinets in a sheet metal factory warehouse.
1.3. What Goes Inside the Frame
The usable parts of a rack are simple but numerous. Vertical mounting rails carry the equipment and must match the 19-inch hole pattern with square holes, threaded holes, or a mix for cage nuts. The frame is formed from steel channel sections with a top and base for stiffness, leveling feet or casters, and removable side panels on an enclosure. Cable organizers, trays, and rear bars keep fibers and copper under control, while PDU brackets and a grounding stud complete the structure. A small 9U wall-mount rack contains more than twenty fabricated parts; a 42U cabinet with doors, rails, shelves, and cable management contains several hundred.
1.4. Quality Is Judged the Moment a Rack Arrives
The rack is the first thing a technician sees and the last thing the facility touches, so its quality is judged immediately. Doors must open and close smoothly, hinges must stay aligned for years, panels must line up without gaps, and the powder coated surface must survive tools and sliding server cases. The dimensions matter even more: if the two front rails are not spaced correctly, or the front and rear rails are not aligned, the equipment will not fit. That is why serious rack brands treat the frame as a precision product rather than a commodity box.
1.5. Customization and the Partner Model
Customization is part of the product story. OEM and ODM brands need different depths for different server generations, door styles such as glass, solid, or perforated, different locks, custom colors, silk-screened branding, and freight-ready packaging. Some customers need earthquake-rated frames with extra bracing; others need a low-cost standard cabinet for a school network room. XHX Metal, the English brand of Guangdong Xinghaoxin Technology Co., Ltd., is a privately owned sheet metal company in Dongguan with a 2,000-square-meter factory, 28 production machines, two 6 kW fiber lasers, and an annual capacity of about 500,000 parts. The sections below walk through usage, materials, production, lead time, and real projects so buyers know what to prepare.
2. Usage Characteristics: How Server Racks Are Used in the Field
2.1. Data Center Rows
Data centers are the most demanding users. Racks are arranged in hot aisle and cold aisle rows, so the cabinet must work with the airflow plan: vented front doors, perforated rear doors, blanking panels to stop recirculation, and sometimes a duct for hot air. High-density installations put heavy equipment in the lower U positions and use sliding rails, cable arms, and vertical PDUs. Technicians constantly pull servers in and out, so the rails must hold equipment securely while the frame stays square. A clean powder coated finish that does not shed particles and grounding continuity on every metallic part complete the data center requirement.
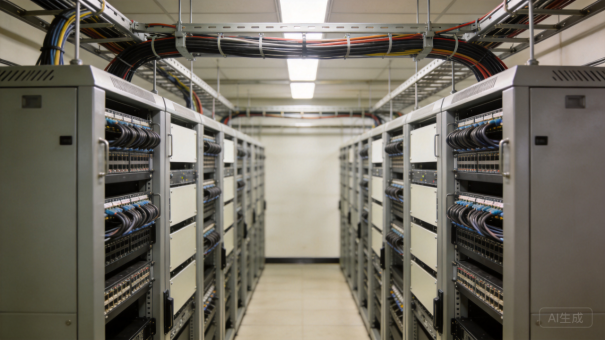
Enterprise data center network room with rows of 42U steel server cabinets.
2.2. Network Rooms and Telecom
Network closets and telecom rooms are where two-post racks and wall-mount racks dominate. In an office closet, a 19-inch rack holds patch panels, switches, routers, and a UPS in a small space with limited depth. Wall-mount racks save floor space but need strong anchors, so the frame must be light enough to install and strong enough to carry the gear. In telecom exchanges, relay racks carry heavy copper and fiber bundles, and cable management must protect bend radii. Humidity, dust, and temperature swings are common, so the finish and hardware matter even indoors.
2.3. Edge Computing and Industrial Sites
Edge and industrial sites add vibration, dirt, and heat. A network rack on a factory floor may sit next to machines, so it needs a lockable door, filtered ventilation, and a frame that does not flex when forklifts pass. Semi-outdoor sites such as base stations push the design further with galvanized or aluminum parts, weather seals, higher IP ratings, and stainless fasteners. Even an indoor rack must survive shipping: fully assembled units and flat-pack kits both stress the frame, so welds, joints, and packaging are designed for the trip as well as the final room.
2.4. Load, Safety, and Grounding
Load capacity is a usage characteristic buyers often misunderstand. A rack has a static load for equipment standing still and a dynamic load for transport or movement on casters. A standard 42U four-post rack may be rated for 800 to 1,500 kg, but the real rating depends on the rail gauge, fastener count, frame design, and base. In earthquake zones the rack must be bolted to the floor and braced, so the base and brackets need anchor strength. Grounding and bonding connect every door, panel, and rail, which protects technicians and helps electromagnetic compatibility; some customers add conductive or anti-static coating inside.
Fire safety and physical security also shape daily use. Racks in public or mixed-use buildings may need lockable doors, tamper-resistant hardware, and materials that meet local fire regulations. Access from the front or rear affects aisle width and door swing, so the drawing should state which side technicians use and how much clearance the doors need.
2.5. Turn Usage Into Specification
The practical lesson is that usage should be written into the specification before fabrication. Depth, door style, perforation, load, cable management, lock type, and finish are all usage decisions, and each one changes the sheet metal design. A rack destined for a sealed data center aisle differs from a wall-mount unit in a dusty factory closet. When the usage is clear at the drawing stage, material and process choices become easier, and the finished rack performs the way the buyer expected instead of becoming a field problem.
3. Material Characteristics: Choosing the Right Steel for Rack Hardware
3.1. Cold Rolled Steel: The Workhorse
Cold rolled steel is the backbone of the server rack industry. Rolling at room temperature gives it a smooth surface, consistent thickness, and good dimensional accuracy, which makes it ideal for precision bending and painted products; grades such as SPCC appear in frames, doors, and panels across the market. It has high strength and excellent plasticity, so it can be formed into complex channel profiles without cracking, and it welds well with standard MIG and TIG processes. Its weakness is corrosion: bare cold rolled steel rusts easily, so every part must receive full pretreatment and powder coating, and scratches through the coating need touch-up. For well-painted indoor racks, it is usually the best balance of performance and cost.
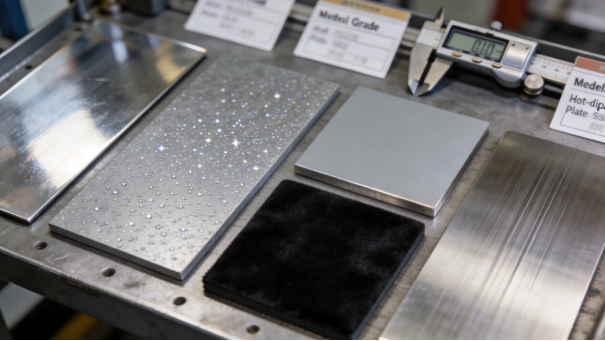
Sheet metal material samples, calipers, and grade tags on an inspection workbench.
3.2. Galvanized Steel: Corrosion at a Fair Price
Galvanized steel is cold rolled steel coated with zinc, usually by hot-dip galvanizing, and it is chosen when corrosion resistance matters more than surface uniformity. The zinc layer protects the steel at a reasonable cost, so galvanized sheet is common for back panels, internal brackets, cable trays, and budget enclosures. Fabrication requires two precautions. Sharp bends can crack or flake the zinc, so bend radii should be generous and the bend area inspected. Welding galvanized steel produces zinc fumes, so the workshop needs ventilation, and the weld area should be cleaned and re-coated afterward. Many manufacturers use galvanized steel as a substrate and powder coat the visible parts, combining corrosion protection with a uniform color.
3.3. Stainless Steel and Aluminum: Selective Upgrades
Stainless steel serves the harshest environments. Grades 304 and 316 form a self-healing chromium oxide layer that resists moisture, chemicals, and salt, and 316 adds molybdenum for coastal and medical duty. It is heavier, harder to cut and bend, and more expensive, so it is used selectively: visible frames in premium medical or lab products, coastal installations, outdoor telecom cabinets, and hinges, locks, and fasteners. Aluminum takes the opposite path: it weighs about one-third as much as steel, resists corrosion naturally, and forms and welds well in alloys such as 5052 and 6061. Aluminum is ideal for doors, profiles, and sliding shelves, while steel remains the safer frame material for heavy loads. The best rack design is often a steel frame with aluminum accessories.
3.4. Gauge, Strength, and Cost
Sheet thickness is the second dimension of material selection. Cabinet panels are usually 1.0 to 1.5 mm, internal brackets and mounting plates 1.5 to 2.0 mm, and load-bearing rails and bases 2.0 to 3.0 mm or more. Mounting rails must carry servers without deflecting, so the gauge, bend profile, and fastener count matter more than the raw material grade. A good fabricator suggests a lighter gauge where the frame geometry provides stiffness and a heavier gauge where the customer specifies a high static load. Cost should be compared on finished parts rather than price per kilogram, because density, scrap, processing time, and finishing all change the final price.
3.5. Finishes That Make It Last
Powder coating is the standard finish for indoor racks because it is tough, uniform, and available in any RAL color. The process starts with cleaning and chemical pretreatment, usually zinc phosphate or chrome-free conversion coating, followed by electrostatic application and oven curing. Outdoor or industrial designs may add an anti-corrosion primer, a textured finish that hides scratches, or a conductive internal coating for grounding continuity. Surface treatment is where material characteristics become product performance: the right coating keeps a rack looking professional for years, while the wrong one turns a good frame into a field complaint.
4. Production Difficulty: Precision, Distortion, and Tolerance Control
4.1. Why Tolerance Is Everything
Server racks look simple but are difficult to produce because the dimensional requirements are strict. The 19-inch standard fixes the mounting width at 482.6 mm, the front rails sit 465 mm apart between hole centers, and every U position along each rail must line up with the others. If the frame is twisted, the doors will not close, the rails will not accept the servers, and the cabinet becomes scrap. Controlling squareness, twist, and hole position through cutting, bending, welding, and finishing is the core difficulty, and it is why cheap racks fail in the field while well-made frames last for years.
4.2. Laser Cutting and CNC Bending
Production starts with laser cutting. XHX Metal uses two 6 kW fiber laser machines that cut panels, rails, brackets, and doors with positioning accuracy of about 0.01 mm, nesting parts to save material and producing edges that need deburring. The cutting stage must be precise because every later step depends on it: a mounting hole out of position on the flat pattern becomes a larger error after bending. CNC bending then turns the sheet into three-dimensional parts. The press brake operator accounts for bend allowance, springback, and grain direction, and the machine must repeat the same angle across the batch. Sharp bends can crack galvanized coating, so tooling radius and material grade are matched to the angle.
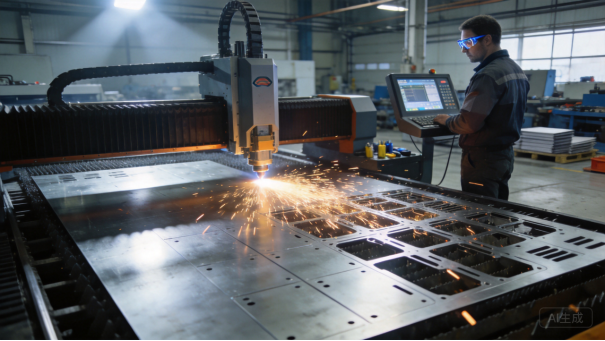
Fiber laser cutting of steel sheet for server rack panels.
4.3. Welding Without Distortion
Welding is the highest-risk step. The frame and rails are joined with TIG, MIG, or laser welding, and heat always tries to distort the steel; long thin frames are especially sensitive because welding one side can pull the whole structure out of square. The solution is controlled process: dedicated jigs, tack welding, a defined weld sequence, and alternating sides so the heat balances. XHX welds joints in a fixed order, then checks the diagonal measurements of every frame. If a frame is not square after welding, no finishing process can fix it, so this check is not optional.
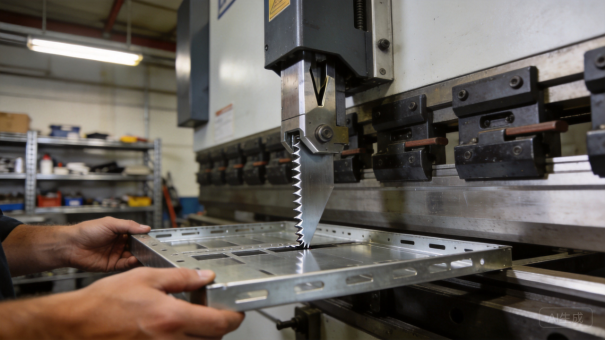
CNC press brake forming a steel panel for a server rack frame.
4.4. Assembly and Hardware
Assembly adds another layer of precision. Vertical mounting rails are fixed with rivets, bolts, weld nuts, or PEM fasteners, and the left and right rails must sit at the same height and depth. Doors hang on hinges that must align with the frame, locks must line up with strike plates, and grounding studs must attach to every metallic panel. Some racks use tapped holes, others use square holes with cage nuts, and the choice changes tooling and assembly time. A one-millimeter error can make a door rattle or a server slide unevenly, so hardware fit is checked as carefully as sheet metal dimensions.
4.5. Coating, Inspection, and Control
Finishing makes the difficulty visible. Powder coating adds thickness, and too much coating around mounting holes prevents hardware from fitting, so threaded areas, grounding points, and labels are masked and parts are hung to avoid pooling in corners. After coating, every batch is inspected for dimensions, squareness, door fit, surface quality, and hardware function. XHX performs first article inspection on every new design and full inspection on visible and functional features, and documents results so a batch can be traced back to its material certificate. Production is also a scheduling problem: cutting is fast, bending is medium, welding is slow, and finishing is the bottleneck, so the factory sequences orders so panels flow without waiting.
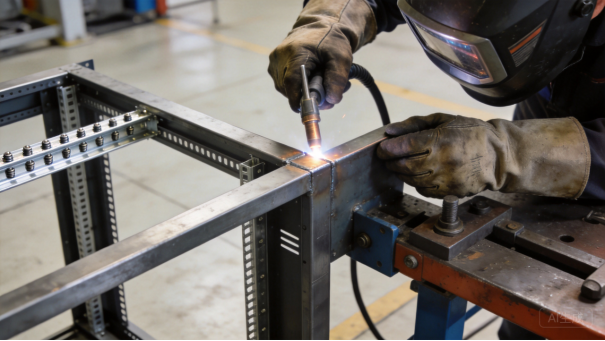
TIG welding and assembly of a 19-inch server rack frame on a jig.
5. Lead Time: From Drawing to Shipped Server Rack
5.1. Realistic Timelines
Lead time is usually the second question a rack buyer asks, after price, and it has the most variables. A completely new rack design typically needs four to eight weeks from approved drawings to delivered production, including a first article. A repeat order of an established design can ship in two to four weeks. The real schedule depends on the design, the material, the finishing process, the order quantity, and the shipping method, so the stages below give a practical breakdown instead of a single magic number.
5.2. DFM Review and Material Procurement
The cycle starts with design review and quotation. When XHX Metal receives a 3D model and 2D drawing, the engineering team checks material, thickness, bend radii, hole patterns, tolerances, finishes, and hardware, and flags anything difficult to produce; this DFM review takes one to three working days. Material procurement follows, with standard cold rolled and galvanized steel available from local suppliers in one to three working days. Special orders, such as pre-painted steel in a custom color or stainless steel with mill certificates, take longer. Because steel prices move, the quotation carries a material validity period, and the specification should be frozen when the order is placed.
5.3. Prototype and First Article
Prototyping comes next. For a new rack design, XHX produces a first article within one to two weeks after material arrives, including laser-cut and formed frame parts, welded and deburred components, and usually a trial powder coat so the customer can verify dimensions, color, texture, and fit. Special bending tools, forming dies, or welding jigs add a few days to two weeks. The customer’s approval of the first article is the green light for production; changes requested at this stage extend the timeline, which is why a complete drawing saves money and weeks.
5.4. Production and the Finishing Bottleneck
Mass production runs in batches. For 100 to 1,000 racks, production usually takes one to three weeks depending on process count and finishing capacity. The factory sequences cutting, bending, welding, deburring, and surface treatment so parts flow without waiting, and QA checks the first and last parts of each shift to catch drift early. Two laser cutters and multiple press brakes mean one maintenance event does not stop an order. Powder coating is the bottleneck: cleaning, pretreatment, spraying, and curing take longer than cutting and bending, and masking for threaded holes and grounding points adds hours. The scope matters too, since some buyers take raw parts while others receive fully assembled cabinets with doors, hinges, locks, rails, and grounding kits.

Powder coated server rack panels and doors on the finishing line.
5.5. QC, Packaging, and Shipping
The final days are quality control and packaging. XHX inspects dimensions, squareness, door fit, and surface quality, prepares packing lists and material certificates, and protects racks with corner protectors, film, and bracing so they survive freight. From Dongguan, air freight to North America or Europe takes about three to seven days, while sea freight to a major port takes three to five weeks plus customs and inland delivery. The company’s on-time delivery record is 93.1 percent on the Alibaba international platform. Practical advice for buyers: freeze the design, approve the first article quickly, and order spare doors or rails with the main run, because a small reorder later costs much more.
6. Past Cases: Server Rack Projects We Have Built
6.1. How to Read These Cases
Project examples show how usage, materials, production difficulty, and lead time come together. Because customer confidentiality is part of XHX Metal’s service, the cases below are described without brand names, but they represent real rack projects produced by the company in recent years, with quantities and timeframes taken from actual order records. The projects cover different regions, rack families, and finishing systems to show how the same process adapts.
6.2. Case 1: 42U Data Center Cabinets for a North American ISP
An internet service provider needed enclosed cabinets with 1,000 mm depth, vented front doors, and a high static load rating for colocation customers. The previous supplier delivered frames that twisted during welding, so doors did not align and servers bound on the rails. XHX redesigned the frame with corner gussets, changed the welding sequence to balance heat, and added a squareness check on the assembly fixture. The first article was approved in eight working days, and 300 cabinets shipped over four weeks. The customer reported that assembly time dropped noticeably because rails and doors fit without adjustment. A written first article report with photos, measured dimensions, and coating checks was approved before the production batch started.
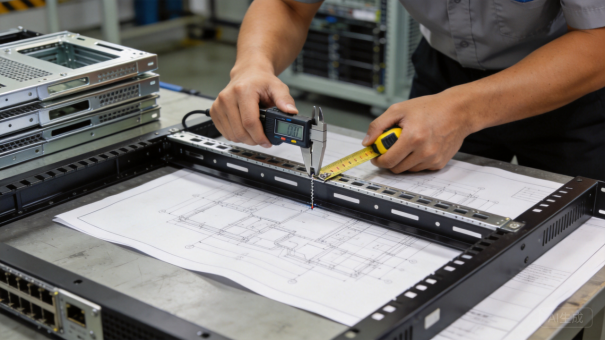
Quality inspection of server rack mounting rail spacing before shipment.
6.3. Case 2: Telecom Relay Racks for Southeast Asia
A telecom contractor building network rooms in a humid tropical market needed two-post relay racks and wall-mount racks in one family design. The key requirements were low cost, corrosion resistance, and simple installation in rooms with limited depth. XHX supplied galvanized steel frames with powder coated finishes, stainless fasteners, and standardized cable management bars. The pilot batch passed humidity and salt spray testing, and about 1,200 units shipped in three batches over eight weeks.
Packaging was standardized for tropical freight: corner protectors, moisture-resistant film, and pallet bracing cut transit damage, and the smaller wall-mount units were nested to save container space. The contractor reused the same packing plan for later projects.
6.4. Case 3: Compact Edge Cabinets for a European Integrator
An IT integrator deploying edge nodes in shops, factories, and offices needed a compact 24U cabinet with 650 mm depth, a tempered glass front door, and rear cable access. XHX reviewed the design for bend and weld details, delivered a prototype within ten working days, and followed with monthly production batches. The most valuable changes came from the DFM review: simplified cable entry cutouts, standardized hinge spacing, and a pre-drilled grounding stud position that worked at every installation. Field feedback from the first installs also confirmed that the rear cable access saved time during commissioning, so the design was kept for the production series.
6.5. Case 4 and the Lessons We Reuse
A networking brand wanted a family of racks from 9U wall-mount to 47U floor cabinets with the same finish, hardware, and packaging. XHX standardized the rail profile, hinge kit, lock, and cable management across the family, which reduced tooling and cut unit cost after the first months; the brand now receives mixed container loads with different heights and door options. The consistent lessons are simple: DFM review prevents assembly problems, material and finish must match the environment, welding and bending consistency makes a design repeatable, first article approval protects the schedule, and quick decisions from a private company keep projects moving. The brand also reports fewer damage claims because the standardized packaging and bracing were tested across every height in the family.
7. Summary: What to Prepare Before Starting a Server Rack Project
7.1. Start With the Engineering Package
The engineering package matters most when starting a rack project. It should include the 3D model and 2D drawing, material grade and thickness, load rating, mounting rail specification, door and lock style, finish color and texture, cable entry points, grounding requirements, packaging method, and target volume. Even a short DFM checklist answered in one email can save a week of back-and-forth later, because fabrication decisions depend on details that are cheap to change on paper and expensive to change after cutting.
Before sending files, list the questions that matter most to your design: maximum static load, door style, cable routing, and target color are usually enough to start a DFM conversation. The supplier can then confirm what is standard and what needs custom tooling.
7.2. State Standards and Finishes
Standards should be explicit. Most rack projects follow the 19-inch EIA-310 and IEC 60297 conventions, but the buyer must confirm the U count, hole pattern, rail spacing, depth, and tolerance. The drawing should also define the surface: powder coating color and thickness, masking points, and grounding continuity. If the rack will live outdoors or in a coastal area, the material and finish specification must be upgraded before fabrication, not after a field failure. A one-line note about the environment prevents the most expensive mistakes.
7.3. Agree on the Commercial Package
The commercial package is equally important. Confirm the delivery incoterm, inspection standard, payment schedule, material validity period, and rules for design changes. Ask for a first article schedule, a production capacity statement, and a list of certifications. ISO 9001:2015, CE, and SGS verification are useful signals, but the practical proof is how quickly the supplier answers a drawing question and how carefully it documents a batch. A supplier that explains its process is easier to trust than one that only promises a date. Written confirmation of the delivery date, inspection points, and packaging standard prevents disputes once the order is in production.
7.4. Why Work With XHX Metal
XHX Metal suits this kind of project because it is a privately owned company with production control in one place. The owner and engineering team can approve tooling changes, discuss material substitutions, and agree on a realistic delivery date without passing decisions through a distant headquarters. The factory has two 6 kW fiber laser cutters, CNC bending and welding, an automatic deburring line, CNC machining, and a 500,000-part annual capacity, which is enough for mid-volume rack programs and flexible enough for prototype runs.
7.5. The Next Step
The fastest way to start is to send your drawings and ask for a DFM review and quotation. XHX Metal can confirm the material route, finish system, production difficulty, and realistic lead time within a few working days. Contact Barry at +86 13244963694 or sales01@xinghaoxin.com, or visit https://www.xhxmetal.com. The factory is at No. 42 Changtang Avenue, Yantian, FengGang Town, Dongguan, Guangdong, China. IT infrastructure will keep evolving toward higher density, liquid cooling, and more sustainable materials, but the frame still has to be square, strong, well finished, and on time, and that is exactly what a controlled sheet metal process delivers. Quotes and DFM comments are usually returned within two working days, and FOB, CIF, and DDP options are available so the logistics can be planned together with production.
Material Comparison for Server Rack Components
| Material | Strength | Corrosion Resistance | Typical Rack Use |
| Cold Rolled Steel (SPCC) | High | Poor unless painted | Frames, doors, panels, internal rails |
| Galvanized Steel (SGCC) | Moderate to High | Good | Back plates, internal parts, budget enclosures |
| Stainless Steel 304/316 | High | Excellent | Coastal, medical, and visible hardware |
| Aluminum Alloy 5052/6061 | Moderate | Good | Doors, profiles, shelves, lightweight accessories |
About XHX Metal
XHX Metal (Guangdong Xinghaoxin Technology Co., Ltd.) is a privately owned sheet metal fabrication company in Dongguan, Guangdong, China. The company specializes in producing and processing sheet metal enclosures and frames for the data center, telecommunication, networking, and industrial equipment sectors, with two 6 kW fiber laser cutting machines, CNC bending, TIG, MIG, and laser welding, an automatic deburring line, CNC machining, and ISO 9001:2015 quality management.
Contact: Barry | +86 13244963694 | sales01@xinghaoxin.com | https://www.xhxmetal.com